Study optimises Material Extrusion parameters for sintered copper parts
Published:
Republished by Newlife - MIM. All rights belong to the original publisher; see Source below.
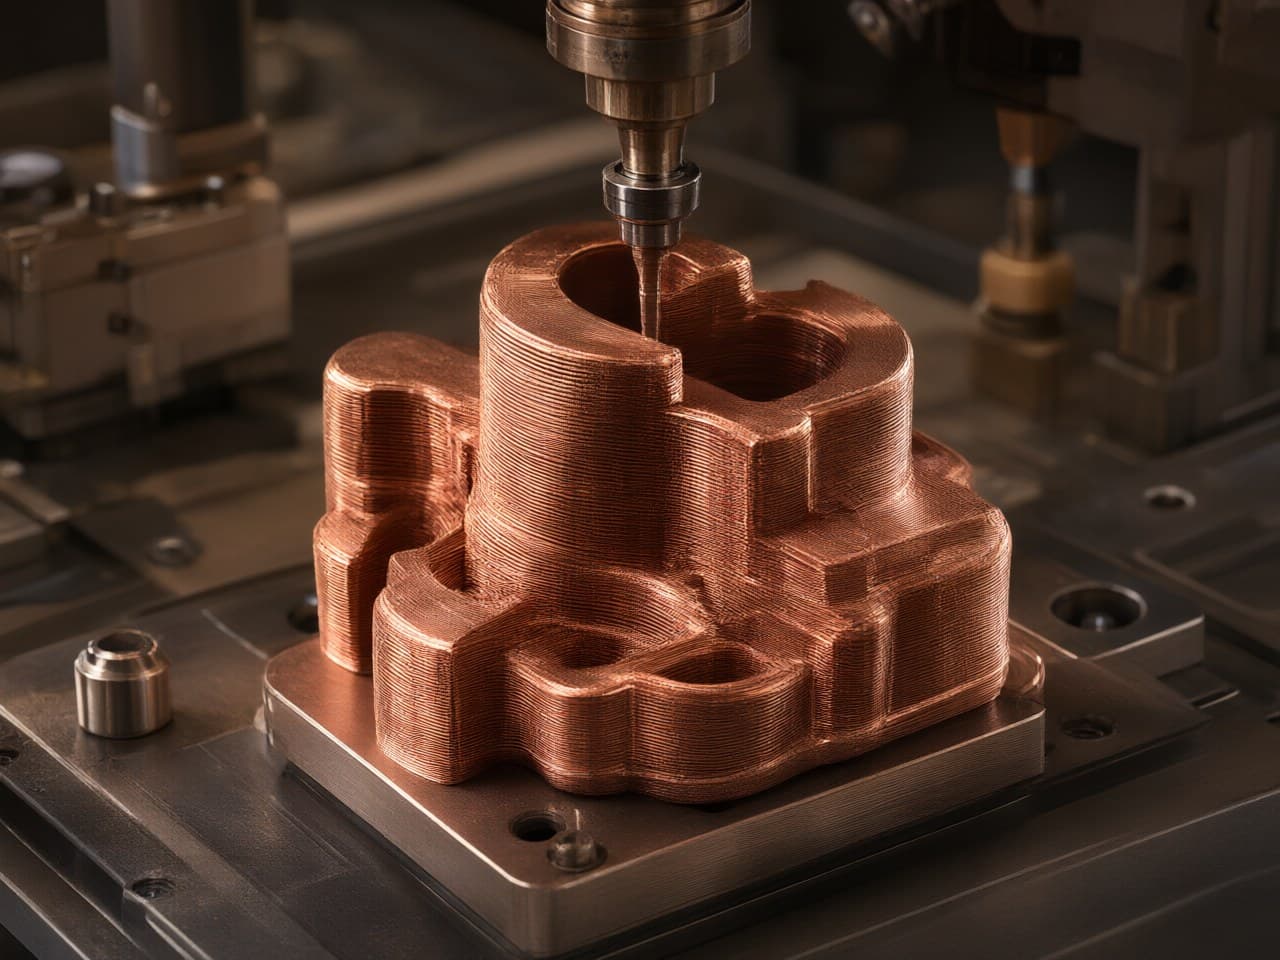
Researchers from the University of Foggia, Italy; the Polytechnic University of Bari, Italy; and the Slovak University of Technology in Bratislava have published a study in Progress in Additive Manufacturing investigating the optimisation of Material Extrusion (MEX) process parameters for the Additive Manufacturing of copper parts using highly filled filament.
The researchers examined the effects of layer height, flow rate and overlap percentage on parts produced from filament containing 87–90 wt.% copper with PLA binder. A design of experiments (DoE) approach was used to assess green density, sintered density, defect formation, pore distribution and shrinkage.
In the green state, a layer height of 0.30 mm, flow rate of 100% and overlap of 15% produced the highest green density, 88.6%. This parameter set was designated the best green combination (BGC). Increasing the layer height to 0.45 mm resulted in a slight reduction in green density, while overlap percentage was found to have no significant effect.
Following thermal debinding, the researchers reported weight losses of 0.7–2.4%. Average dimensional changes of +0.2%, +0.1% and +1.5% were recorded along the x-, y- and z-axes, respectively.
The highest sintered density, 90.4%, was achieved using a layer height of 0.45 mm, a flow rate of 90% and an overlap of 20%. This condition was designated the best sintered combination (BSC). As with the green parts, overlap percentage was reported to have little influence.
The BGC and BSC samples were further evaluated using X-ray computed tomography (CT) to examine internal voids. The BSC samples contained a relatively uniform distribution of numerous small pores attributed to the printing stage. The BGC samples contained fewer voids overall, but included larger isolated voids attributed to the sintering stage, which the researchers stated were likely to be more detrimental to material properties.
Mechanical characterisation also included hardness and tensile testing. According to the study, increasing flow rate improved green density; however, higher green density did not translate directly into improved sintered density, with internal and external defects beginning to appear as green density increased.
The researchers concluded that optimisation of the complete MEX Additive Manufacturing process chain is required to minimise defects in sintered copper parts. Further work will focus on identifying practical printing and sintering windows capable of balancing density, dimensional accuracy, part integrity and surface quality.
‘Systematic methodology to manufacture and validation of copper parts via material extrusion technology’ is available here.
Source
- pim-international.com (2026-10-04) - Original article: Study optimises Material Extrusion parameters for sintered copper parts - https://pim-international.com/study-optimises-material-extrusion-parameters-for-sintered-copper-parts